Sustainability
LOWEST-CARBON
ALUMINUM
EXTRUSIONS
Lowest carbon aluminum extrusions ever produced in history – by design, with the very first billet pushed.
NEAR-ZERO SCOPE 3 CARBON FOOTPRINT
Our Process design
Low‑carbon aluminum extrusions — by design, not offsets
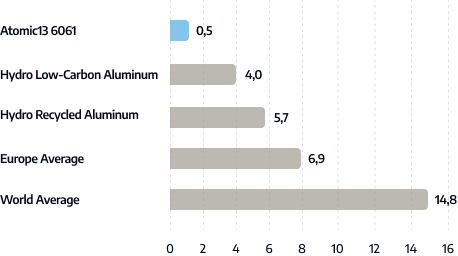
Atomic13 manufactures high-performance extrusions from 100% post-consumer scrap (PCI + twitch) with no primary aluminum for unwanted element dilution. Our total embodied carbon footprint is ~0.5 kg CO2e / kg Al produced versus the next lowest carbon product on the market which is ~4.0-4.2 kg CO2e / kg Al produced from a conventional extruder. That’s ~90% lower embodied carbon achieved through process design, not achieved through off-set credits.
Note: Metrics are based on LCA estimates using the ‘cut-off method’ defined in ISO 14064 / 14067.
METHODOLOGY
What We include
CLEAR DEFINITIONS BASED ON INDUSTRY ACCEPTED STANDARDS FOR CALCULATION:
For Scope 3 (raw material input contributions to carbon footprint) the ISO-defined ‘cutoff method’ is the standard used by A13 for the calculation.
SUSTAINABILITY CERTIFICATION:
- Start with third-party Life Cycle Assessment (LCA) of the process to define true carbon for Scope 3 raw material inputs to the process.
- With the LCA in place, next define the EPD (Environmental Product Declaration with support from a third party). This process officially defines A13’s carbon footprint in accordance with generally accepted US standards (Scope 3 and Scopes 1 and 2).
- Prepare and conduct third-party audits to the ASi (Aluminum Stewardship Initiative) Performance Standard and receive certification.
- Evaluate our supply chain partners up and downstream. Prepare and conduct third-party audits to achieve the ASi Chain of Custody certification which certifies the A13 supply chain.
- ASi promotes responsible production, sourcing and stewardship in the aluminum industry, setting sustainable standards for the entire value chain. Environmental, social governance and good corporate citizenship (ESG) criteria focused on climate change initiatives, biodiversity and human rights are covered by the standard. A13 believes in doing our part to enhance the quality of life not only for our employees, but for the residents of the communities where we operate.
PROCESS DESIGN THAT LOWERS CO2 EMISSIONS:
For Scope 3 carbon footprint, the raw material inputs produced from 100% post-consumer scrap is a major differentiator from the competition. For Scope 1 and 2 carbon footprint which are essentially associated with efficiency of energy use within the process, A13 beats competitors by eliminating the need to heat treat billets after casting (homogenization). Because heat is naturally generated from material internal friction related to shear, we do not need to heat billets to high temperatures prior to extrusion which saves energy and reduces carbon.
Why it matters
sustainability outcomes by sector

Humanoid Robotics / Robotics

Automotive & EV

Defense & Aerospace
TRANSPARENCY & COMPLIANCE
Verification & Reporting

EPDs
Third‑party verified, cradle‑to‑grave disclosures that report the environmental impacts of a product across its life cycle for our product families.
Our methods of calculation are carefully vetted through established ISO standards and conservative methods of calculation are used. A13 is careful to avoid ‘green washing.’

LCAs
ISO 14040 / 14044-compliant life-cycle assessments are systematic, science-based methods for evaluating environmental impacts of our product and process across its entire life cycle – from raw material extraction to end-of-life in service. LCAs support our internal carbon accounting and are critical to understanding the impact of our company on the environment where we operate.

Traceability & recycled content
Recycled content attestations per sustainability certification status can be included on material test reports upon request.
Benchmarks
Simple math customers can use

0.5 kg
CO₂/kg billet at scale
Benchmark:
Lowest‑carbon industrialized conventional billet ≈ 4.2 kg CO₂e/kg.
Atomic13:
≈ 0.5 kg CO₂e/kg (calculated according to ISO 14040 / 14044 standards)
Program impact:
Every 10,000 metric tons of billet shifted to Atomic13 avoids roughly 37,000–40,000 t CO₂e vs. low‑carbon conventional—
and significantly more vs. primary.